The Complete Guide to Anti-Corrosion Coatings for Steel Structure Buildings: Primers, Topcoats, and Coating System Selection
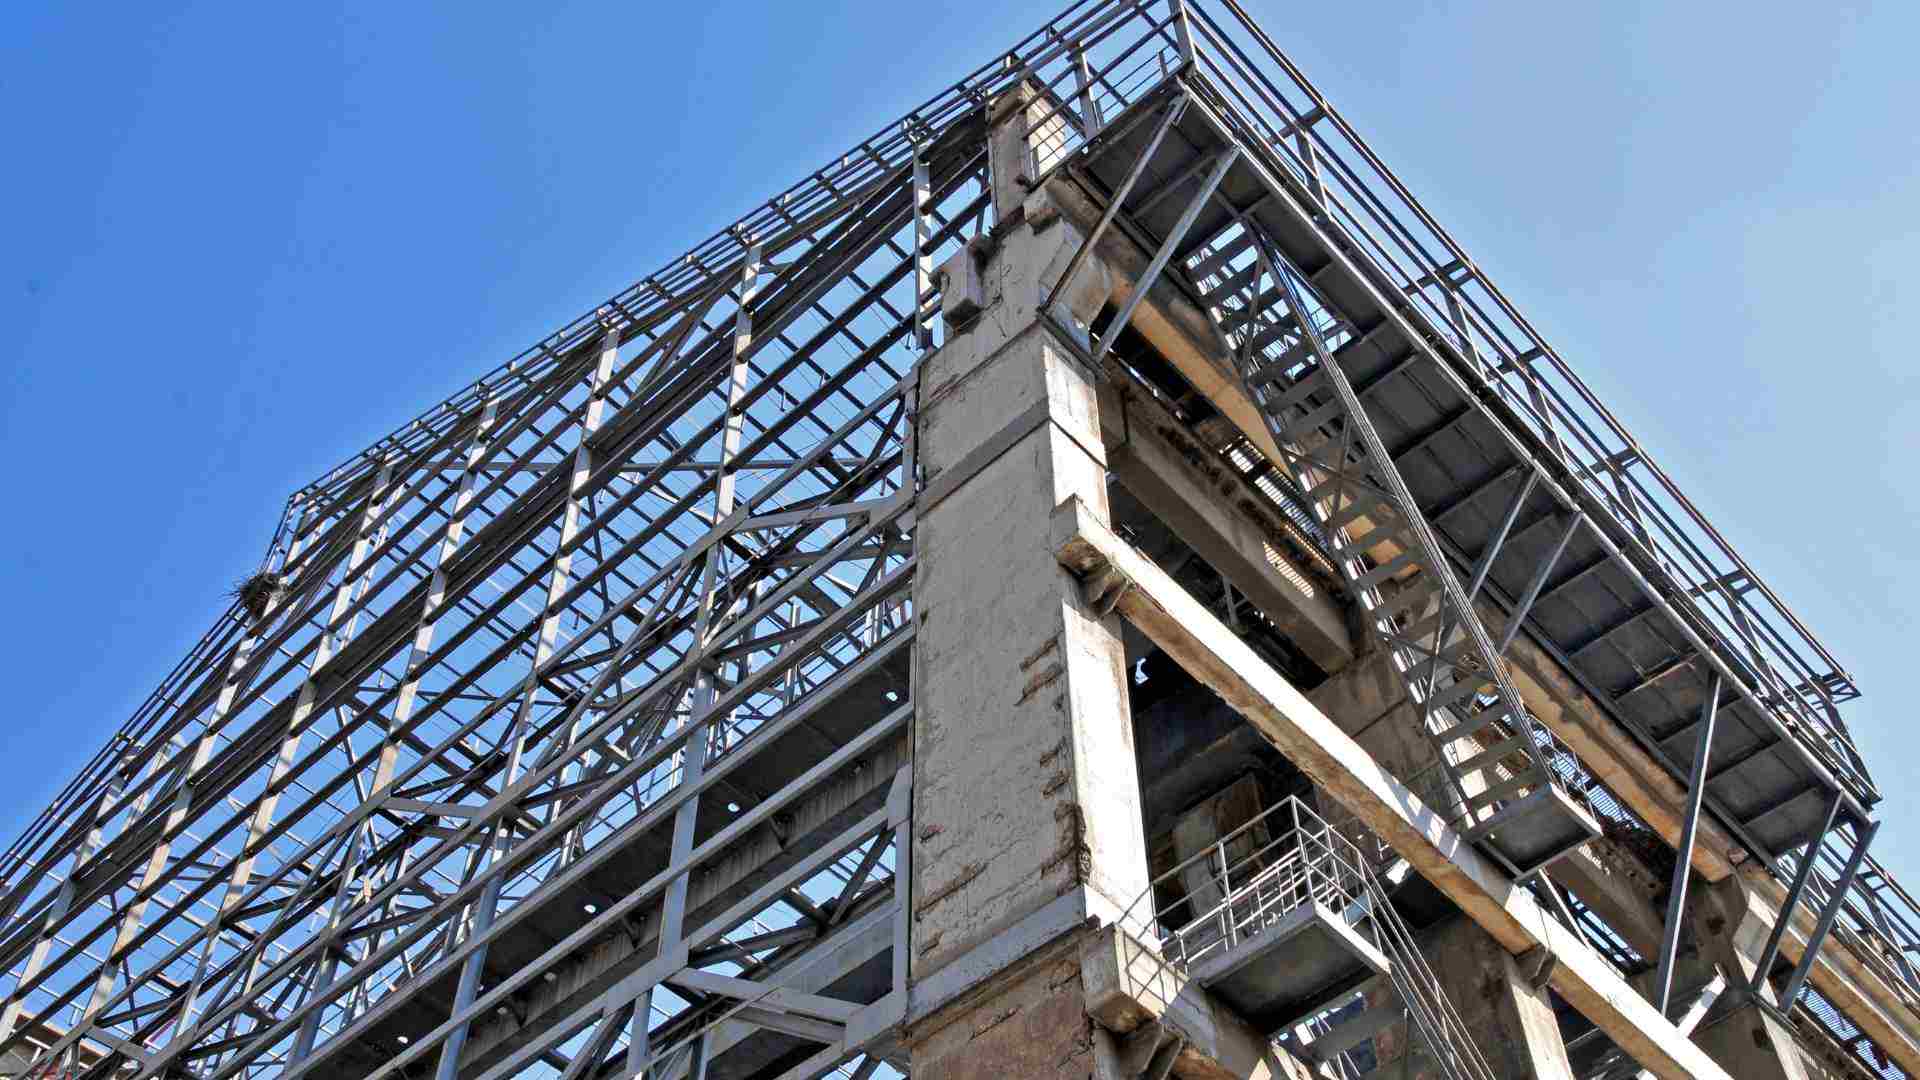
Steel is one of the most durable and versatile building materials available, but it has a well-known vulnerability: corrosion. Left unprotected, structural steel begins to oxidize the moment it is exposed to moisture and oxygen. In coastal environments, industrial zones, or regions with high humidity, that process accelerates dramatically. A steel beam that could serve for a century with proper protection might show visible rust within months without it.
The solution is not a single coat of paint. Professional corrosion protection for steel structures relies on a multi-layer coating system — typically a primer, an intermediate coat, and a topcoat — where each layer performs a distinct function. Understanding how these layers work together is essential for anyone involved in constructing, maintaining, or renovating a steel building, whether it is a warehouse, a workshop, an agricultural facility, or a commercial structure.
This guide walks through the fundamentals of anti-corrosion coatings systems for steel buildings: what each layer does, which products are best suited to different environments, how surface preparation affects everything, and how to choose a system that balances performance with budget.
Why Steel Corrodes — and Why a Single Coat Is Never Enough
Corrosion is an electrochemical process. When steel is exposed to water and oxygen, iron atoms lose electrons and form iron oxide — rust. The process is self-reinforcing: rust is porous and holds moisture against the steel surface, accelerating further oxidation. Salt, industrial pollutants, acid rain, and even soil contact intensify the reaction.
A single layer of paint can slow this process temporarily, but it cannot stop it. Every coating film contains microscopic imperfections — pinholes, thin spots at edges and welds, areas where the film was applied unevenly. In a single-coat system, each of these imperfections is a direct pathway for moisture to reach the steel. Once corrosion initiates at these weak points, it spreads beneath the coating, causing blistering, flaking, and eventually structural section loss.
Multi-layer systems solve this problem through redundancy. The primer bonds directly to the steel and provides initial corrosion resistance. The intermediate coat builds film thickness and creates a dense barrier. The topcoat shields the entire system from ultraviolet radiation, weathering, and chemical exposure.
If one layer has a defect at a particular point, the layers above and below it compensate. This is why international standards like ISO 12944 treat corrosion protection as a system-level design decision rather than a product selection.
Layer One: The Primer — Your First Line of Defense
The primer is the most critical layer in any anti-corrosion coatings system. It must bond tenaciously to the prepared steel surface and provide the initial barrier or sacrificial protection that prevents corrosion from starting. There are three main categories of primers used on steel structures, and the right choice depends on the environment, the expected service life, and the rest of the coating system.
Zinc-Rich Primers
Zinc-rich primers are the gold standard for high-performance corrosion protection. They work on the principle of cathodic (galvanic) protection: the zinc particles in the primer are more electrochemically active than steel, so they corrode preferentially, sacrificing themselves to protect the substrate. This mechanism is the same principle behind hot-dip galvanizing, but delivered in a paintable form.
There are two sub-types. Inorganic zinc-rich primers use an ethyl silicate binder and provide the highest level of corrosion resistance. They are extremely hard, heat-resistant, and durable, but they require careful surface preparation (typically near-white metal blast cleaning to SSPC-SP 10 or equivalent) and controlled application conditions. Organic zinc-rich primers use an epoxy binder, are more forgiving to apply, and cure faster, making them popular for field applications and fabrication shops.
Zinc-rich primers are the standard choice for steel structures in coastal, marine, industrial, and high-humidity environments — essentially any setting classified as C4 or C5 under ISO 12944 corrosivity categories.
Epoxy Primers
Epoxy primers provide excellent adhesion and chemical resistance. Rather than sacrificial protection, they rely on barrier performance — creating a dense, cross-linked film that physically blocks moisture and contaminants from reaching the steel.
Epoxy primers are widely used in moderately corrosive environments (ISO 12944 categories C2 and C3) and are often chosen for interior steel, enclosed structures, or situations where zinc-rich primers are impractical.
One important limitation: epoxy primers (and epoxy coatings in general) are not UV-stable. Exposed to sunlight, they will chalk, fade, and eventually degrade. This is why an epoxy primer is almost never used as a standalone exterior coating — it needs a UV-resistant topcoat over it.
Alkyd and Modified Alkyd Primers
Alkyd primers are the most economical option, offering acceptable corrosion protection in mild environments with low humidity and minimal chemical exposure. They dry quickly and are easy to apply, making them suitable for interior steel or structures that will be enclosed within a controlled environment.
However, their chemical resistance and long-term durability are significantly lower than zinc-rich or epoxy alternatives, and they are rarely specified for exterior-exposed or mission-critical steel.
Layer Two: The Intermediate Coat — Building the Barrier
The intermediate coat (sometimes called the build coat or midcoat) sits between the primer and the topcoat. Its primary function is to add film thickness and create a dense, impermeable barrier that reinforces the protection provided by the primer.
High-build epoxy coatings are by far the most common choice for this layer. Applied at dry film thicknesses of 125 to 200 microns per coat, they create a tightly cross-linked barrier that resists moisture penetration, chemical attack, and mechanical abrasion.
The intermediate coat also serves as a buffer that prevents any chemical incompatibility between the primer and the topcoat — a real concern when combining zinc-rich primers with certain topcoat chemistries.
In standard three-coat systems, the intermediate coat is typically specified in a contrasting color to the primer. This is not an aesthetic decision — it is a quality control measure. When the topcoat is applied over a differently colored midcoat, any areas of insufficient topcoat coverage become immediately visible, allowing inspectors to catch and correct thin spots before the structure enters service.
Layer Three: The Topcoat — UV Protection, Weathering Resistance, and Appearance
The topcoat is the outermost layer of the coating system and the one exposed to the harshest conditions: ultraviolet radiation, rain, temperature cycling, airborne contaminants, and mechanical wear. Its job is to protect everything underneath it while also delivering the desired appearance — color, gloss, and texture.
Aliphatic Polyurethane Topcoats
Polyurethane topcoats are the most widely specified finish for exterior steel structures. Aliphatic polyurethanes, in particular, offer outstanding UV resistance, excellent color and gloss retention over years of outdoor exposure, and good chemical resistance. They are the standard topcoat in the classic three-coat system (zinc-rich primer, epoxy intermediate, polyurethane topcoat) that dominates industrial and commercial steel construction worldwide.
Polyurethane topcoats are classified under SSPC Paint 36 by their UV resistance duration, giving specifiers a clear framework for matching performance to project requirements. For steel buildings expected to maintain their appearance for fifteen to twenty-five years before recoating, an aliphatic polyurethane topcoat is typically the most cost-effective choice.
Polysiloxane Topcoats
Polysiloxane (siloxane-modified) topcoats represent a newer technology that offers even greater durability than polyurethanes in some applications. They combine the flexibility of organic coatings with the hardness and UV resistance of inorganic silicone chemistry.
Polysiloxane topcoats can achieve equivalent or better performance than polyurethanes with fewer coats and lower total film thickness, potentially reducing application time and cost on large projects.
They are increasingly popular for large-scale steel structures — bridges, power plants, stadiums — where recoating access is expensive and minimizing maintenance cycles has significant economic value.
Acrylic Topcoats
Water-based acrylic topcoats are gaining traction for projects with strict volatile organic compound (VOC) regulations or where low-odor application is required. Modern acrylics offer good color retention and weathering resistance, though they generally do not match the chemical resistance or abrasion durability of polyurethanes. They are well suited for steel structures in urban environments where environmental compliance and indoor air quality are priorities.
Choosing the Right Coating System for Your Steel Building
Selecting a coating system is not about picking the most expensive products available — it is about matching the system to the environment, the expected service life, and the building’s functional requirements.
The international standard ISO 12944 provides a structured framework for this decision by classifying environments into corrosivity categories (C1 through CX) and linking them to recommended coating system types and minimum dry film thicknesses.
For a steel warehouse or workshop in a dry, inland, temperate climate (C2), a two-coat system of epoxy primer and polyurethane topcoat may be entirely sufficient. For a coastal agricultural building (C4 to C5), a full three-coat system with a zinc-rich primer is typically the minimum specification. For offshore or heavy industrial applications (CX), specialized systems with metallic thermal spray or multi-coat zinc and epoxy systems may be required.
Beyond performance, the topcoat is also where building owners make aesthetic decisions. The range of available colors for metal buildings has expanded significantly in recent years, with manufacturers now offering dozens of standard and custom shades formulated with UV-stable pigments specifically designed for steel cladding and structural members.
Selecting the right color is not just a matter of brand identity or curb appeal — lighter shades reflect more solar radiation, reducing thermal load on the building envelope, while darker colors may require higher-performance topcoat formulations to resist accelerated UV degradation and chalking.
When evaluating coating system options, property owners should request documentation of the complete system specification — not just individual product data sheets, but the full primer-intermediate-topcoat build, including recommended dry film thicknesses per layer, surface preparation standards, recoat intervals, and expected service life under the specific environmental conditions of the project site.
Surface Preparation: The Step That Determines Everything
No coating system, regardless of cost or quality, can outperform poor surface preparation. Industry data consistently shows that the majority of premature coating failures trace back to inadequate surface prep rather than defective products. The primer can only bond to what it touches, and if that surface is contaminated with mill scale, rust, grease, dust, or moisture, the bond will fail.
Abrasive blast cleaning is the standard preparation method for new structural steel. The process removes mill scale and creates a rough surface profile that gives the primer mechanical grip. Near-white metal blast cleaning (SSPC-SP 10 / NACE No. 2) is the most commonly specified grade for high-performance systems, achieving approximately 95 percent removal of all visible contaminants. White metal blast cleaning (SSPC-SP 5 / NACE No. 1) is specified for the most demanding applications, such as immersion service or inorganic zinc primer application.
For existing structures being repainted, surface preparation requirements depend on the condition of the old coating. Spot repairs may only require localized power tool cleaning (SSPC-SP 3 or SP 11), while full recoating typically calls for sweep blasting to achieve a suitable profile over the existing sound coating. In all cases, solvent cleaning (SSPC-SP 1) to remove oil and grease should be the first step — before any mechanical preparation.
One critical detail that is often overlooked: stripe coating. Edges, welds, bolt heads, and other irregular surfaces are inherently difficult to coat evenly with spray equipment. Stripe coating — applying an additional brush coat of primer and intermediate to these areas before or after the full spray coat — is essential to ensure adequate film thickness at the points most vulnerable to corrosion initiation.
Application and Quality Control
Even with the right products and proper surface preparation, the coating system can still fail if application is poorly executed. Environmental conditions during application matter enormously. Most coating manufacturers specify minimum and maximum application temperatures (typically between 50°F and 100°F), maximum relative humidity (usually below 85 percent), and a minimum margin above the dew point (typically at least 5°F) to prevent moisture condensation on the steel surface during coating application.
Dry film thickness (DFT) measurement is the single most important quality control activity. Each layer of the system has a specified DFT range, and the total system build must meet the overall specification. DFT is measured with magnetic or eddy current gauges at multiple points across the structure, with particular attention to edges, welds, corners, and other areas where thin spots are most likely.
Recoat windows also demand close attention. Every coating product has a minimum and maximum recoat interval — the time window during which the next layer can be applied and achieve proper intercoat adhesion. Applying too soon, before the previous coat has cured sufficiently, can trap solvents and cause blistering. Waiting too long can result in the previous coat becoming too hard and smooth for the next layer to bond, requiring mechanical abrasion to restore adhesion.
Maintenance and Recoating: Protecting Your Investment Over Time
A well-specified and properly applied coating system is not a permanent solution — it is a long-term one. All coating systems have a finite service life, and planning for maintenance from the outset is far more cost-effective than waiting for visible failure.
Regular visual inspections should be scheduled at least annually, with more frequent checks in aggressive environments. The earliest signs of coating degradation — chalking, minor rust spotting at edges, hairline cracking — are far easier and cheaper to address than full-scale delamination or significant steel section loss. Spot repairs using compatible products can extend the overall system life by years.
When full recoating becomes necessary, the economics favor systems that were well maintained. A structure with an intact primer and intermediate coat may only need topcoat renewal, a far less expensive proposition than stripping back to bare steel and rebuilding the entire system. This is another reason why the initial coating specification matters so much — a robust three-coat system with a zinc-rich primer may cost more upfront, but it provides a foundation that supports decades of cost-effective maintenance.
The Bottom Line
Anti-corrosion coatings are not an afterthought in steel construction — it is a structural protection system that deserves the same engineering attention as the steel members themselves. The choice of primer, intermediate coat, and topcoat must be driven by the specific environmental conditions of the project, the targeted service life, and a realistic understanding of maintenance access and budgets.
For property owners and builders, the key takeaway is straightforward: specify the system, not just the product. Understand the environment. Invest in surface preparation. Insist on quality control during application. And plan for maintenance before the first coat dries. Steel buildings are designed to last for generations. The right coating system ensures they actually do.